Verified electro-acoustic engineering platforms, certified under rigorous international quality protocols for commercial distribution, OEM audio brands, and enterprise volume procurement.
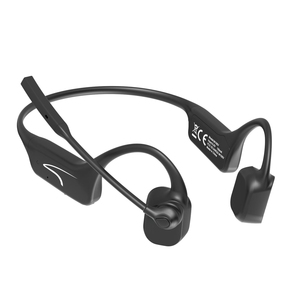
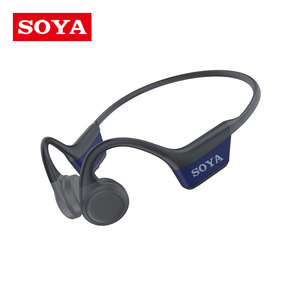
Quantifiable manufacturing benchmarks validated through third-party factory audits and international quality certifications.
Why leading global brands, electronics distributors, and enterprise buyers partner with our certified manufacturing hubs for high-performance subwoofer components.
In-house acoustic simulation labs equipped with Klippel R&D systems and AP (Audio Precision) analyzers. We engineer voice coils, spider compliance, and cone damping to deliver maximum SPL with under 0.5% Total Harmonic Distortion (THD).
Every transducer design undergoes rigorous environmental validation: 65°C thermal soak tests, salt-mist spray exposure, monsoon humidity cycling, and continuous 14-hour duty cycle stress trials to guarantee thermal stability under high load.
Comprehensive manufacturing white-label programs including private tooling, custom voice-coil impedance optimization, enclosure acoustic matching, silk-screen logo application, customized retail packaging, and tailored firmware UI integration.
In the rapidly evolving landscape of global audio engineering, securing a trusted subwoofer speaker factory and exporter requires an in-depth analysis of transducer mechanics, thermal management capabilities, and electro-acoustic alignment. Subwoofer drivers serve as the foundation for low-frequency sound reproduction across diverse applications, ranging from professional sound reinforcement and automotive audio to premium consumer soundbars, open-ear wearable audio, and smart home theater ecosystems. Unlike mid-range or high-frequency transducers, subwoofers operate under extreme mechanical stress and high displacement requirements, demanding rigorous engineering standards from raw material selection to final quality assurance.
When enterprise procurement teams and OEM brands audit manufacturing partners, the primary focus centers on Thiele-Small (T/S) parameters engineering, voice-coil heat dissipation efficiency, dynamic excursion limits, and structural enclosure integration. A factory's ability to maintain tight tolerance controls over $Q_{ms}$ (mechanical quality factor), $Q_{es}$ (electrical quality factor), $F_s$ (resonant frequency), and $V_{as}$ (equivalent compliance volume) directly dictates the acoustic output consistency across mass production runs. Top-tier exporters integrate automated laser displacement testing (such as Klippel analyzer systems) directly into their assembly lines to measure cone excursion linearity ($K_{x}$) and force factor linearity ($BL(x)$) in real time.
Furthermore, international compliance has expanded beyond standard electrical safety. Global export protocols demand that premium subwoofer speaker factories maintain full compliance files covering BIS certification for regional distribution, CE markings for European markets, FCC compliance for North America, and RoHS compliance for environmental hazardous substance control. Advanced manufacturing facilities back their hardware platforms with a robust global service infrastructure, establishing warranty fulfillment targets, local spare-parts stocking, and direct firmware updates for smart connected audio systems.
As consumer preferences shift toward high-efficiency, multi-functional, and ultra-compact audio solutions, procurement managers must align their supply chain strategies with emerging manufacturing trends. The global loudspeaker and transducer industry is undergoing a structural transition driven by digital signal processing (DSP) hardware coupling, lightweight magnetics, and sustainable material science. Understanding these procurement vectors allows B2B buyers to select manufacturing partners capable of supporting next-generation product roadmaps over a 5 to 10-year horizon.
Traditional subwoofer designs relied heavily on bulk ferrite magnets to generate the flux density required for low-frequency cone control. Modern procurement trends show an exponential shift toward high-grade Neodymium-Iron-Boron (NdFeB) magnet assemblies. Neodymium motors provide significantly higher magnetic flux per unit of weight, enabling factories to engineer compact, ultra-lightweight subwoofers suitable for open-ear wearable audio, portable PA systems, and slim automotive enclosures without sacrificing magnetic field strength or sensitivity.
Hardware alone no longer dictates subwoofer performance. Modern procurement contracts increasingly specify co-developed DSP firmware. Exporters now provide integrated Class-D amplifier boards paired with customized DSP algorithms that enforce dynamic excursion limiting, virtual bass synthesis, room equalization, and thermal protection. By dynamically adjusting filter coefficients based on real-time driver impedance feedback, modern subwoofers achieve deeper low-frequency extension without risking mechanical bottoming out or thermal coil burnout.
Environmental regulatory pressure and corporate ESG initiatives are reshaping raw material sourcing within speaker factories. Leading exporters are moving away from traditional synthetic plastic cones toward bio-composite membranes, recycled bamboo fiber pulp, thermoformed TPU surrounds, and eco-friendly resin binders. These sustainable materials are engineered to match or exceed the specific stiffness-to-weight ratio and internal damping properties of traditional polypropylenes, ensuring low cone breakup distortion while meeting strict international environmental directives.
To assist procurement directors and audio systems engineers in evaluating driver architectures, the following matrix outlines the key mechanical, thermal, and electrical specifications across core subwoofer factory configurations:
| Transducer Architecture | Voice Coil Topology | Magnet Material | Nominal Excursion ($X_{max}$) | Frequency Range ($F_s$) | Target Application |
|---|---|---|---|---|---|
| Micro-Subwoofer Transducer | Single CCAW (Copper-Clad Aluminum) | NdFeB N45H High-Temp | ± 2.5 mm | 65 Hz - 3.5 kHz | OWS / Wearables / Smart Glasses |
| Compact Enclosure Subwoofer | Dual 4-Layer High-Temp Kapton | Ferrite Y35 High-Flux | ± 8.5 mm | 35 Hz - 500 Hz | 2.1 & 5.2 Dolby Soundbars |
| High-Excursion Pro Subwoofer | 4-Inch Edge-Wound Copper Wire | NdFeB N52 Vented Motor | ± 18.0 mm | 22 Hz - 250 Hz | Pro Audio / Cinema Subwoofers |
| Automotive Flat-Profile Sub | Dual Voice Coil (DVC) Aluminum Former | High-Grade Strontium Ferrite | ± 12.0 mm | 28 Hz - 400 Hz | In-Vehicle Under-Seat Enclosures |
The global audio industry is witnessing an unprecedented convergence between traditional acoustic physical dynamics and advanced digital sound control. Factory R&D centers are spending millions to break physical acoustic barriers, achieving higher sound pressure levels (SPL) from progressively smaller enclosure volumes. Five critical engineering developments define current subwoofer production lines:
1. Advanced Thermal Soak and Heat Dissipation Geometry: Voice coil thermal failure remains the leading cause of field returns in subwoofers. Advanced factories now implement radially vented pole pieces, black anodized aluminum formers, and forced-air cooling channels integrated directly into the driver basket. These structural thermal management techniques lower operating temperatures by up to 25°C during continuous peak power playback, preventing thermal power compression and preserving magnet efficiency.
2. Linear Suspension Optimization via Finite Element Analysis (FEA): Using non-linear FEA simulation software, acoustic engineers optimize the geometry of spiders and surrounds. By creating progressive-rate spiders and dual-roll surrounds, factories eliminate asymmetrical mechanical damping. This structural symmetry ensures that forward cone displacement matches rearward cone displacement precisely, dramatically lowering odd-order harmonic distortion ($THD_3$).
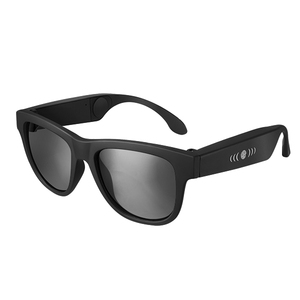
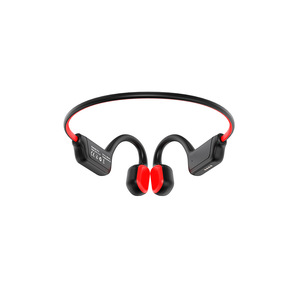
3. Open-Ear Air Conduction and Directional Subwoofer Modules: Micro-subwoofer technology has expanded beyond static enclosures into personal wearable devices. Open-Ear OWS headphones and smart audio sunglasses now feature micro-subwoofer modules capable of delivering punchy tactile bass response while utilizing reverse-phase acoustic cancellation channels to prevent sound leakage into neighboring environments.
4. Smart Active ANC and Dynamic Low-End Tracking: Integrating active noise cancellation (ANC) into low-frequency audio systems requires precise driver response matching. Subwoofer driver factories are designing specialized low-latency voice coils that respond instantaneously to ANC phase-inversion signals, effectively neutralizing ambient cabin noise in automotive applications and low-frequency rumble in aviation environments.
5. Automated Robotic Assembly and Quality Assurance: Leading exporter factories have transitioned from manual gluing lines to fully automated robotic assembly cells. High-precision dispensers apply UV-curing adhesives to voice coil, cone, and spider joints with sub-millimeter accuracy. Automated vision systems inspect surround alignment, while automated AP stations perform 100% sweep-frequency testing for Rub & Buzz defect isolation before final packing.
Selecting a manufacturing partner involves evaluating operational resilience, quality control management systems, and post-purchase engineering support. A top-tier OEM/ODM partner operates with a systematic workflow designed to eliminate product vulnerabilities prior to mass distribution:
Our strategic manufacturing infrastructure is built upon four foundational pillars: Strict Material Traceability, Comprehensive Accelerated Lifecycle Testing, Full Compliance Program Verification, and Dedicated B2B Turnkey Support. Every batch of copper magnet wire, spider material, cone pulp, and magnet assembly is documented and tracked. Transducers are subjected to accelerated lifetime testing involving hundreds of continuous hours under pink noise at rated AES power within environmental chambers set to extreme temperature and humidity configurations.
Furthermore, our dedicated corporate procurement program supports complete customization from low-level voice coil winding impedance modifications to custom-molded tooling, firmware UI branding, packaging design, and localized logistics fulfillment. With established service capabilities spanning over 200 cities globally, distribution partners benefit from rapid claim processing, structural spare-parts stocking, and direct engineer-to-engineer technical consultation.
Our certified manufacturing facilities specialize in five core hardware lines: Personal Audio Transducers (ANC TWS earbuds, open-ear OWS headsets, bone conduction sport earphones, micro-subwoofer drivers), Smart Wearables (AMOLED, rugged outdoor, and fitness smartwatches), Automotive Recording Electronics (4K dashcams, dual-channel and 3-channel fleet systems), Home Audio (2.1 to 5.2 channel Dolby soundbars with active subwoofers), and Smart Projection Hardware (Google TV and 4K HDR optical engines).
Yes. All hardware platforms carry full compliance files for global distribution. Products are BIS certified for Indian regional distribution and carry complete CE, FCC, and RoHS documentation for European and North American markets. Select home audio soundbars and smart projection systems feature licensed decoding technologies, including official Dolby Audio and Netflix certification.
We provide comprehensive OEM/ODM turnkey engineering services. Qualified volume orders can utilize custom plastic/aluminum injection tooling, bespoke voice coil winding specifications, custom enclosure tuning, logo silk-screening, custom retail packaging design, and firmware-level UI adaptation. Technical engineering teams manage projects from initial CAD/3D modeling through tooling validation and mass production sign-off.
Every transducer unit undergoes 100% automated acoustic sweeps using Audio Precision software to detect frequency response deviations, total harmonic distortion (THD), phase anomalies, and Rub & Buzz defects. Batches undergo accelerated thermal soak testing above 65°C, high-humidity exposure, drop and vibration profiling, salt-mist corrosion checks, and multi-day continuous duty cycle power handling trials.
We support all production platforms with a 12-month standard manufacturer warranty. B2B partners access a service network spanning over 200 cities globally, featuring a target 5-day claim turnaround time. We stock functional spare parts (voice coils, crossover boards, amplifier modules, power supplies) across the complete active product lifecycle.
Standard evaluation samples for existing platforms ship within 3 to 5 business days upon request qualification. Standard production MOQs start at 1,000 units for standard hardware colors and configurations, while fully custom OEM/ODM private mold projects typically carry an MOQ of 3,000 to 5,000 units depending on tooling complexity.
Connect directly with our electro-acoustic engineering team to request product samples, factory audit documentation, technical datasheets, or custom OEM/ODM volume pricing schedules.
Contact Us